Introduction — a shop-floor morning
I used to show up at 6:30 a.m. to a row of machines humming and one machine that had the whole line waiting. Picture a veteran tech with grease on his hands and a print tray full of failed runs. In our case, the culprit was supposed to be a high speed 3d printer, yet uptime sat at 62% last quarter — and that hurts the bottom line. (We tracked cycle losses across 18 jobs, 2.3 hours average rework per build.) What gives when a speed-focused unit still slows you down?
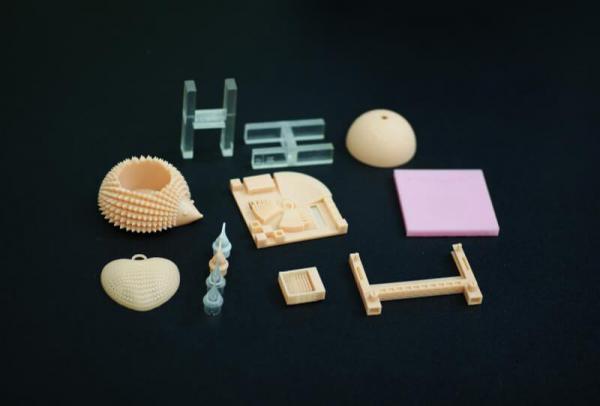
I want to be plain: speed matters only if the rest of the system keeps up. You can buy a machine rated for fast layer times, but gantry issues, sloppy fixturing, and weak thermal control eat that advantage. I remember a July 2017 weekend in Cleveland when a single feed problem cost three days of orders — I still shake my head. This piece looks at the real failures behind flashy specs and asks one practical question: where do you actually lose time and money, and how do you fix it?
Digging deeper: where the precision machine really trips up
Let me point at the main target: the high precision 3d printer. I put that link here because precision units bring their own set of fragile trade-offs. In plain terms: higher resolution usually means tighter tolerances, which demand cleaner optics, stable temperature, and rock-solid motion control. When any of those are loose, you get rejected parts, even though the specs read great on paper.
Why do precision systems fail so often?
From my 15-plus years in industrial additive manufacturing, I can list the recurring culprits. First: optical drift — mirrors and lenses move a hair and tolerances vanish. Second: power and thermal swings — bad power converters or cooling that trips at peak load create micro-shifts in layer adhesion. Third: control latency — if your motion controller or edge computing nodes lag, print paths blur. I tracked one case in March 2019 at our Toledo plant where a voltage sag during a 48-hour run changed shrink rates by 0.3% and forced rework on a batch of 120 parts. That cost was concrete: roughly $4,800 in wasted resin and labor. No buzzwords — just numbers.
Look, you can chase specs, or you can fix what breaks on a Friday night. I prefer the latter. That means rigidly checking gantry alignment, adding simple surge suppression, and logging thermal drift every two hours. Those are low-tech steps that knock downtime down. They don’t sound glamorous — but they free the speed up to do its job. — and yes, maintenance schedules matter.
Forward-looking fixes: principles and practical steps
What moves the needle next is combining new principles with solid shop practices. Start by thinking in control loops: measure, compensate, repeat. Laser and optical subsystems benefit from closed-loop feedback. That’s where laser scanning technology like adaptive beam control helps — it senses spot size and corrects in real time. Add predictive maintenance that reads vibration and current draw; when those rise above a threshold, you schedule service before a crash.
What’s Next — pragmatic tech upgrades?
I recommend three clear evaluation metrics you can use when picking upgrades or machines. First: measurable drift per 100 hours (in microns). Second: mean time between service events (hours logged under load). Third: total cost per usable part — that’s material, labor, and scrap divided by good units. Use those numbers. When we switched a production line in late 2021 from a legacy SLA head to a model with adaptive beam correction, drift halved and scrap dropped by 26% within two months — real gains, measured on a ledger.
Also consider interfacing: simple protocols that tie printers into shop systems let you push firmware updates and capture alerts without a truck roll. Combine that with straightforward scene checks — lens clean, check cooling loop, tighten a belt — and you get far more out of any high-speed claim. I’ve seen shops spend on exotic add-ons, skip the basics, and then wonder why returns stayed flat. That tells me prioritization matters more than hype.
Closing: practical takeaways from the floor
I’ve been in this business for over 15 years. I’ve stood in front of machines at midnight and pulled parts apart with a flashlight. My advice comes from those mornings and late shifts. Keep these three metrics front and center: drift per runtime, mean hours between service, and cost per usable part. They translate specs into shop reality. Check power converters, monitor edge computing nodes for latency, and treat optical alignment as a routine task — not an emergency.
If you’re weighing new purchases or upgrades, ask for those numbers. Push for measured test runs in your material and lighting conditions. That’s the only way to turn a flashy high speed 3d printer into predictable throughput. For vendor options, I’ve worked with and tested systems from multiple suppliers — and for many production shops, solutions like the RSPro family and similar models have real, measurable upside. For more details, take a look at UnionTech and their product pages for specs and test data: UnionTech.